Mastercam vs camworks stands at the very heart of modern manufacturing innovation, where raw metal transforms into precision engineering through the sheer power of advanced digital logic. Across bustling workshop floors and high-tech design rooms alike, brilliant minds continuously debate which platform holds the ultimate key to unlocking peak productivity. Every single keystroke and calculated toolpath represents a delicate balance between blazing-fast execution speeds and absolute mechanical safety.
Behind the glowing computer screens, powerful algorithms wage a silent war to conquer complex geometry, intricate multi-axis movements, and stubborn metal alloys. Engineers and machinists pour their expertise into mastering these sophisticated ecosystems, turning abstract CAD data into breathtaking physical realities. As industries push the absolute boundaries of what CNC machines can achieve, choosing the right digital toolkit becomes the defining factor between ordinary production and extraordinary manufacturing excellence.
Machinists frequently evaluate how Mastercam and CAMWorks handle complex multi-axis toolpaths differently on the shop floor
The metallic hum of the workshop floor often carries an unspoken rivalry as programmers debate the nuances of multi-axis machining. Beneath the glowing monitor screens, veteran operators scrutinize how different computer-aided manufacturing platforms interpret raw CAD data to sculpt intricate aerospace components and complex automotive molds. Every rotation of the spindle represents a critical juncture where software intelligence translates into physical reality, demanding absolute precision from the underlying calculation engines.
Mastercam and CAMWorks approach the arduous task of simultaneous five-axis motion through fundamentally divergent computational pathways. Understanding these core algorithmic differences empowers production teams to harness maximum machine efficiency while protecting expensive hardware from catastrophic failures during high-speed material removal sequences.
Algorithmic Foundations of Simultaneous Five-Axis Generation
The generation of simultaneous five-axis toolpaths relies on advanced vector mathematics and curve-fitting algorithms to coordinate linear X, Y, and Z axes with rotational tilt and rotary axes. Mastercam utilizes an expansive suite of proprietary multi-axis engines, such as Blade Expert and Port Expert, which calculate tool orientation by referencing mathematical surface normals and curvature derivatives directly from the solid model.
This approach grants the kernel deep analytical awareness of the part topology, allowing the software to automatically adjust lead and lag angles dynamically across sweeping, undulating geometries without requiring manual point-by-point vector manipulation.
Conversely, CAMWorks operates on a feature-based machining architecture powered by the integrated Dassault Systèmes geometric search engine. When calculating multi-axis routines, CAMWorks scans the solid model for recognized machinable features and applies predefined knowledge-based machining rules to determine tool axis orientation. While Mastercam prioritizes raw mathematical freedom and extensive manual parameter control over surface flow lines, CAMWorks leverages automated feature recognition to dictate tool vector trajectories based on established manufacturing standards.
Both engines translate complex spatial coordinates into smooth, continuous G-code, but they arrive at those synchronized motion vectors through contrasting analytical viewpoints—one driven by geometric decomposition, the other by continuous surface interpolation.
Advanced multi-axis algorithms transform raw mathematical surface data into synchronized, collision-free motion vectors that dictate the physical choreography of the CNC machine.
Geometric Selection Workflows for Rotary Milling Sequences
Executing flawless rotary milling sequences demands a rigorous, highly disciplined approach to geometric boundary selection and drive surface definition. Programmers must carefully orchestrate the interaction between the drive surfaces, check surfaces, and containment boundaries to guide the cutting tool along intricate contours without triggering unexpected axis reversals. The visual workspace displays a virtual symphony of bounding boxes, wireframe containment chains, and highlighted face selections, all working in unison to restrict tool movement to the exact zones requiring material removal.
To achieve seamless multi-axis execution, programmers typically adhere to a structured workflow when defining spatial parameters on the shop floor:
- Isolate primary drive surfaces by filtering out microscopic gaps and tangential discontinuities in the CAD model to prevent erratic tool vector calculations.
- Establish rigid check surfaces surrounding clamps, fixtures, and unmachined stock regions to create an impenetrable digital safety zone around the workpiece.
- Define precise containment boundaries using 3D curves or silhouette edges that dictate the exact entry and exit coordinates for the rotating cutting tool.
- Assign specific tool axis control parameters, establishing whether the cutter should maintain a fixed angle relative to the surface normal, lead by a set degree, or point toward a specific calculated center of rotation.
Boundary Constraint Techniques for Deep Cavity Roughing Passes
Deep cavity roughing operations subject cutting tools to immense mechanical loads and thermal stress, making robust boundary constraint techniques essential for preventing catastrophic tool gouging. When plunging deep into confined pockets, standard clearance planes are often insufficient to protect the tool holder and shank from colliding with steep, vertical walls. Experienced programmers implement strategic stock models and dynamic containment boundaries that evolve with every pass, ensuring the cutting tool only engages un-machined material while maintaining a safe spatial buffer away from critical finished surfaces.
Effective boundary management relies on a combination of digital stock tracking and intelligent air-move suppression to optimize cycle times while securing the workpiece envelope. The following strategies are regularly deployed in high-performance manufacturing environments to safeguard deep cavity roughing operations:
- Utilizing remaining stock models generated from previous operations to automatically restrict toolpath generation strictly to un-cut volumetric zones.
- Implementing multi-depth containment boundaries that step inward and downward progressively, preventing the tool from plunging directly into un-cleared corners.
- Applying negative stock-to-leave values selectively on intermediate roughing passes to ensure smooth transitions before final finishing passes sweep through the cavity.
- Integrating shaft and holder collision checking parameters directly into the roughing boundary definitions, forcing the software to tilt the tool away from vertical walls whenever clearance thresholds are breached.
Comparative Performance Metrics of Advanced CAM Platforms
Evaluating the operational capabilities of Mastercam and CAMWorks requires a comprehensive look at how their output interacts with modern high-speed CNC machinery. The table below Artikels key performance metrics gathered from rigorous shop floor benchmarks across various complex multi-axis machining centers.
| Performance Metric | Mastercam | CAMWorks | Evaluation Context |
|---|---|---|---|
| Maximum Feed Rates | Extremely high, optimized for high-speed contouring | High, integrated with adaptive roughing algorithms | Tested during simultaneous 5-axis aerospace pocketing passes |
| Acceleration Limits | Advanced smoothing algorithms minimize jerk on legacy controls | Rule-based optimization adapts to modern CNC controller dynamics | Measured on high-velocity linear motor gantry machines |
| Post-Processor Reliability | Extensively customizable via MP language, industry-proven | Robust, highly stable output for standard and multi-axis machines | Validated across multi-tasking mill-turn and 5-axis trunnion setups |
| Simulation Fidelity | Comprehensive machine kinematics and material removal verification | Integrated virtual machine environment with real-time collision detection | Cross-referenced with physical first-article inspection reports |
Manufacturing engineers must understand how feature recognition technology alters daily programming routines across both software suites
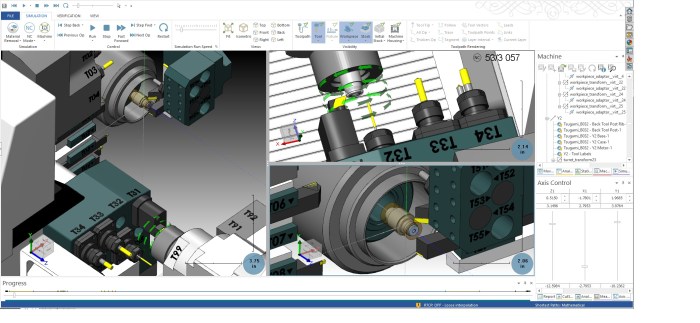
Source: g2crowd.com
The dawn of automated programming has fundamentally reshaped the landscape of modern manufacturing, transforming how engineers approach daily shop floor challenges. Step into any advanced production facility today, and you will witness a quiet revolution driven by intelligent software that reads between the lines of 3D geometry. This shift is not merely about moving faster; it is about redefining precision, minimizing human error, and unleashing human creativity onto more complex engineering hurdles.
Both Mastercam and CAMWorks harness sophisticated computational engines to interpret raw solid models, yet their underlying philosophies regarding automation create distinct daily rhythms for programmers. By decoding intricate design intent straight from the native CAD tree, these platforms liberate programmers from repetitive, click-heavy drafting tasks. The result is a seamless bridge between design engineering and machining execution, where complex geometries are transformed into optimized toolpaths with unprecedented speed and unwavering reliability.
Automated Hole-Making Intelligence Built Into Modern Solid-Based Manufacturing Environments
Hole-making operations traditionally consume a massive portion of programming hours, demanding meticulous calculation of feeds, speeds, depth increments, and tool selections for every single bore. Modern manufacturing environments tackle this bottleneck through automated hole recognition engines that scan solid models to instantly categorize blind holes, through holes, counterbores, and tapped features. When a programmer imports a complex hydraulic manifold containing dozens of interconnected fluid passages, the software instantly identifies the diameter, depth, and thread specifications of each feature without manual measurement.
This automated intelligence goes far beyond simple geometry detection by embedding machinist knowledge directly into the software’s decision-making matrix. Built-in machining databases evaluate material hardness, tolerance callouts, and surface finish requirements to automatically assign the ideal sequence of center drilling, drilling, reaming, and tapping operations. Imagine an aerospace component with three hundred fastener holes of varying depths; instead of manually programming each individual location, the system groups identical features and generates complete toolpath hierarchies in seconds.
Furthermore, collision detection algorithms evaluate tool clearance and holder lengths automatically, ensuring that deep-pocket drilling operations execute safely without manual intervention during simulation.
Advanced rule-based machining takes this a step further by learning from shop floor preferences over time, adapting its default behaviors to match the exact tooling inventory available in the tool crib. If a specific aluminum alloy requires high-velocity peck drilling to manage chip evacuation effectively, the system recalls these parameters instantly upon recognizing the feature attributes. This deep automation dramatically compresses programming cycles from hours to mere minutes, empowering manufacturing engineers to focus on macro-level process optimization rather than getting bogged down in micro-detailing every single hole.
Parametric Solid Modeling Integration Methods That Streamlining Design Change Propagation Into Active Toolpaths
The true test of a robust CAM system lies in its resilience when engineering changes arrive on the shop floor moments before production. Parametric solid modeling integration ensures that when a client updates a bracket’s wall thickness or shifts a mounting hole by two millimeters, the active toolpaths do not break or require manual rebuilding from scratch. Mastercam utilizes robust associativity that links toolpaths directly to solid faces and edges, while CAMWorks leverages feature-based technology rooted in native feature trees to track modifications in real time.
When a design modification occurs, the software visually flags the affected operations, prompting the programmer to execute a rapid regeneration rather than a complete reprogramming session. This associativity preserves previously defined cutting parameters, stepovers, and entry moves, applying them effortlessly to the newly proportioned geometry. Consider a real-world scenario from the automotive sector, where a transmission housing design undergoes a last-minute weight-reduction revision involving pocket depth adjustments.
Parametric integration detects these boundary alterations instantly, recalculating the multi-axis roughing passes to match the new floor depths while maintaining optimal stock-to-leave values.
Choosing Mastercam versus CAMWorks sparks intense debates across modern manufacturing floors, driving engineers to optimize every precision cut. Just as factories rigorously evaluate lca software competitors sphera simapro ecochain 2024 2025 to build sustainable futures, mastering these advanced toolpaths unlocks unprecedented efficiency, empowering visionary machinists to transform raw metal into brilliant masterpieces.
Parametric associativity acts as the invisible safety net of modern CNC machining, transforming sudden engineering revisions from catastrophic delays into minor, automated updates.
Visual verification tools display these updates dynamically, using color-coded comparison overlays to highlight exactly where stock has been added or removed since the last revision. This transparency builds absolute confidence among machine operators, who can initiate production runs knowing that the G-code accurately reflects the absolute latest iteration of the engineering drawing without manual translation errors.
Step-by-Step Procedures for Setting Up Automated Feature Recognition Rules for Prismatic Pocket Milling
Establishing standardized automation rules requires a methodical approach to ensure consistent, reliable toolpath generation across various workpiece geometries. Manufacturing engineers can configure customized recognition parameters to match their shop’s specific machining strategies and preferred cutting tool libraries.
- Access the machining database management portal within the CAM environment to define baseline material libraries, specifying exact Brinell hardness ratings and machinability factors for commonly used alloys like titanium, inconel, and aluminum.
- Navigate to the automated feature recognition settings menu and establish dimensional thresholds for prismatic pockets, defining minimum and maximum depth-to-width ratios that dictate whether roughing or specialized plunging strategies are applied.
- Associate specific tool families with corresponding feature attributes, linking roughing end mills, high-feed cutters, and finishing ball-nose tools directly to predefined pocket geometry classifications.
- Configure strategy rules by assigning preferred stepdown percentages, cutting speeds, and feed rates to specific volumetric removal tiers, ensuring roughing passes maximize material removal rates safely.
- Save the customized rule set as the default template for specific machine groups, enabling consistent application across all incoming prismatic components regardless of which programmer handles the file.
Specific Time-Saving Shortcuts When Processing Imported STEP Assemblies from Various CAD Systems
Importing neutral CAD formats like STEP files from diverse engineering departments often introduces geometry anomalies, overlapping surfaces, and missing metadata that can severely disrupt the programming workflow. Utilizing specialized software shortcuts allows engineers to bypass tedious manual cleanup phases and accelerate the transition from raw CAD data to active, verified G-code.
- Activating the automated solid healing wizard instantly stitches micro-gaps and repairs surface normal inconsistencies imported from external CAD platforms, eliminating manual boundary patching.
- Utilizing the global face-selection filter allows programmers to select all coplanar faces across an entire imported assembly with a single click, instantly suppressing unnecessary holes or chamfers for roughing setups.
- Employing batch-recognition macros applies pre-configured drilling and pocketing rules to multi-part assemblies simultaneously, cutting multi-part setup durations by up to seventy percent in high-mix job shops.
- Applying automatic stock model generation from the bounding box of the imported STEP assembly immediately calculates exact raw material dimensions without manual sketch creation.
- Using intelligent layer-management filters lets engineers instantly isolate internal cooling channels or complex internal cavities from exterior mounting structures, decluttering the workspace for targeted multi-axis programming.
Toolpath verification and machine simulation capabilities dictate the safety limits of high-speed machining centers.
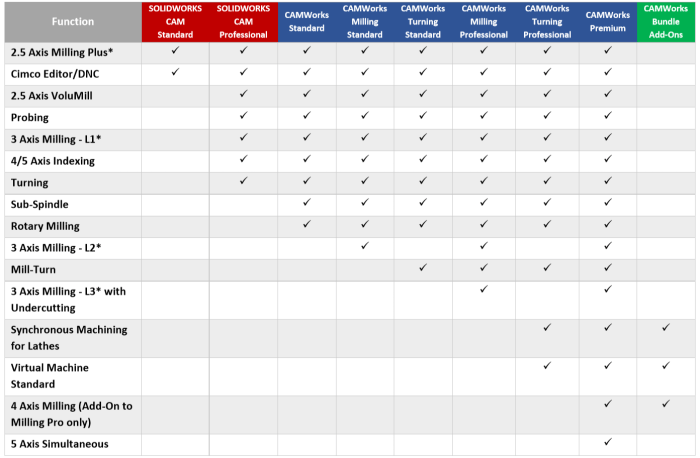
Source: seacadtech.com
On the modern shop floor, the margin for error evaporates the moment a high-speed spindle breaches twenty thousand revolutions per minute. Protecting multi-million-dollar capital investments demands absolute precision before code ever touches metal, shifting the primary burden of security onto advanced digital verification systems.
Modern CAM suites rely on sophisticated internal collision detection engines to shield expensive CNC spindles from catastrophic crashes. These computational safety nets continuously monitor every micro-movement of the tool assembly, holder, fixture, and raw stock throughout complex multi-axis trajectories. By calculating spatial bounding volumes in real-time, the software identifies potential over-travel conditions and near-miss scenarios long before the physical machine executes the block.
When a multi-axis simultaneous move pushes a tool dangerously close to a vise clamp, the detection engine halts execution and flags the exact interference zone in a virtual 3D workspace. This proactive intervention transforms potential workshop disasters into manageable digital revisions.
Material Removal Simulation and Chip Load Realism
Accurate material removal simulation portrays chip load variations during dynamic milling sweeps by visualizing the changing engagement angle of the cutting edge. As high-speed toolpaths sweep through complex pockets, the software renders real-time stock reduction while simultaneously tracking volumetric removal rates. For instance, when profiling aerospace aluminum components with aggressive radial depths of cut, the visual simulation shifts color spectrums to represent fluctuating tool pressures and instantaneous feed rates.
This granular feedback helps programmers spot localized areas of excessive tool engagement where sudden spikes in chip load could cause chatter or premature tool breakage.
Precision digital twinning transforms theoretical G-code into a predictable manufacturing asset, ensuring shop floor safety and absolute execution confidence.
Machine Kinematics Integration and Controller Mirroring
Achieving absolute confidence on the shop floor requires the integration of custom machine kinematics definitions to mirror exact shop floor machine controller behaviors. By embedding the precise axis limits, rotary table pivot points, and kinematic chains of specific hardware into the virtual environment, engineers bridge the gap between office programming and actual machine motion. For example, programming a five-axis mill-turn center requires exact simulation of the sub-spindle clearance zone and tool turret rotation limits to prevent costly interference incidents.
Navigating Mastercam versus CAMWorks requires looking beyond initial licensing fees to embrace adaptive planning ongoing maintenance and support costs , ensuring your machining facility invests wisely in software that drives long-term productivity and operational excellence for every complex milling project.
When the digital twin replicates the proprietary look-ahead processing and acceleration curves of a high-end CNC controller, the resulting simulation accurately forecasts cycle times and axis reversals.
Executing a flawless transition from virtual verification to physical machining requires a disciplined sequence of physical and digital checks. Below are the exact verification steps required prior to dry-running a newly compiled G-code program on the shop floor.
- Execute a complete collision check within the CAM software using fully loaded tool assemblies and exact shop floor fixture models.
- Perform a dry-run in the air with the Z-axis offset elevated well above the stock surface while observing real-time axis coordinates.
- Validate the post-processed G-code file against the specific machine controller parameter manual to eliminate unrecognized canned cycles or illegal block formats.
- Verify work coordinate system and tool length offset measurements directly on the machine control interface using standardized probing routines.
- Run the first operational pass at a reduced feed rate override while keeping a hand resting on the feed hold button for immediate intervention.
Post-processor customization remains a critical bottleneck when deploying new manufacturing software into an established production facility.

Source: ardatadesign.com
Bringing a state-of-the-art CAM platform onto a bustling shop floor often reveals an invisible friction point: the post-processor. Transforming pristine digital toolpaths into the raw, dialect-specific G-code required by aging machine tool controllers is a delicate art that directly impacts daily production flow and machine safety.
Navigating the precision of mastercam vs camworks reveals how crucial efficient toolpath strategies remain for modern manufacturing shops. Much like production floors optimizing workflows, industry leaders must evaluate the shipperguide company 3gtms on freight capacity marketplace to secure reliable logistics networks. Ultimately, mastering these digital solutions guarantees your machining operations achieve peak performance.
When the digital twin meets physical iron, the success of the entire workflow hinges on how precisely the post-processor translates complex multi-axis logic into fluid mechanical motion without risking catastrophic collisions.
Scripting Languages and Template Architectures for Legacy Controllers
Bridging the gap between modern CAM software and older machine controllers demands an intimate understanding of proprietary scripting frameworks and structural template hierarchies. Mastercam relies on MP scripting language, an event-driven environment utilizing specialized post blocks, user-defined variables, and conditional logic to construct output files line by line. Programmers manipulate tokens and post-lines within text-based ASCII files, mapping internal cutter location data directly to customized G-code output.
Conversely, CAMWorks leverages a robust integration built on the Universal Post Generator and ICAM-based technologies, utilizing specialized macro languages and modular template architectures that separate kinematic definitions from formatting logic. Both systems require meticulous attention to detail when addressing legacy iron, as older controllers frequently lack native support for advanced look-ahead buffers or high-order polynomials, forcing the post-processor to linearize complex NURBS splines into dense arrays of micro-segments.
Choosing between Mastercam and CAMWorks shapes modern precision machining paths brilliantly. Just as streamlining campus movement through a minga hall pass unlocks remarkable institutional efficiency, mastering these advanced software giants empowers creators to transform raw digital blueprints into breathtaking metallic masterpieces with absolute confidence and unstoppable technological momentum.
Visualizing this translation process reveals a digital translation engine running tirelessly in the background. Imagine a vast, glowing flowchart within the post-processor environment, where incoming cutter location data cascades through cascading logical gates, filtering out unsupported G-codes, injecting customized tool-change subroutines, and appending precise coolant activations before the final text file is compiled for the shop floor.
Adapting these architectures for specialized shop environments involves configuring custom formatting rules that handle non-standard modal groups and proprietary M-codes unique to custom-built or heavily retrofitted machinery.
Drilling Versus Turning Canned Cycles Modification Complexity
Customizing canned cycles exposes distinct operational philosophies between drilling routines and turning profiles across both manufacturing suites. Drilling cycles typically rely on standardized G-codes like G81, G83, or G73, making the modification of peck depths, dwell times, and retract planes a relatively straightforward exercise in adjusting modal variable assignments within the script. Turning operations, however, introduce significantly higher complexity due to the dynamic nature of variable lead threads, complex grooving profiles, and dynamic roughing cycles such as Fanuc G71 or G72, where single blocks of code control intricate multi-pass material removal geometry.
Engineers modifying turning posts must carefully account for nose radius compensation vectors, tailstock interference zones, and C-axis live-tooling sub-spindle synchronizations, transforming a simple text edit into a rigorous exercise in kinematic verification.
Precision control over machining parameters requires strict adherence to syntax rules when defining cycle outputs, ensuring that machine controllers interpret motion vectors correctly without generating alarm states.
Accurate post-processor customization bridges the vital gap between virtual CAM simulation and predictable shop floor execution.
Post-Processor Development Environment Feature Comparison
Evaluating the underlying toolsets available within each software ecosystem helps manufacturing engineers select the appropriate environment for maintaining legacy equipment and developing robust machine configurations.
| Software Suite | Syntax Editing Tools | Debugging Utilities | Macro Support | Vendor Backing |
|---|---|---|---|---|
| Mastercam | Integrated Code Expert with syntax highlighting and token inspection. | Built-in debugger with variable watch windows and step-through logic execution. | Extensive support for custom user-defined logic, math functions, and conditional post blocks. | Extensive global reseller network alongside direct corporate development support. |
| CAMWorks | Universal Post Generator interface coupled with standard text-based editors. | Step-by-step trace functions and output preview windows for real-time validation. | Robust macro language integration for automating complex turning and milling sequences. | Dedicated technical support teams and specialized post-development engineering partnerships. |
Troubleshooting Methods for Rotary Axis Wind-Up Errors
Simultaneous 5-axis machining often pushes machine kinematics to their absolute limits, frequently resulting in disruptive rotary axis wind-up errors where the C or B axes approach mechanical travel limits mid-cut. Resolving these unorthodox winding phenomena demands systematic troubleshooting methodologies, beginning with a thorough examination of axis limit parameters and shortest-path calculation logic inside the post-processor. Engineers must implement specialized unwind subroutines that detect cumulative angular rotation exceeding three hundred sixty degrees, automatically inserting safe retraction moves, reversing axis positions, and repositioning the tool before resuming the continuous path.
Real-world implementation on dual-rotary trunnion mills demonstrates that pre-calculating vector flips during the post-processing phase eliminates unexpected axis spinning, protecting expensive spindles and cutting tools from destructive mechanical binds during complex multi-sided contouring tasks.
Systematic debugging of these rotational anomalies involves executing dry runs with air cuts while monitoring real-time angular displacement values on the controller screen, allowing operators to catch potential wind-up faults prior to engaging material.
Shop floor scalability and operator learning curves heavily influence the financial investment decisions of manufacturing business owners.
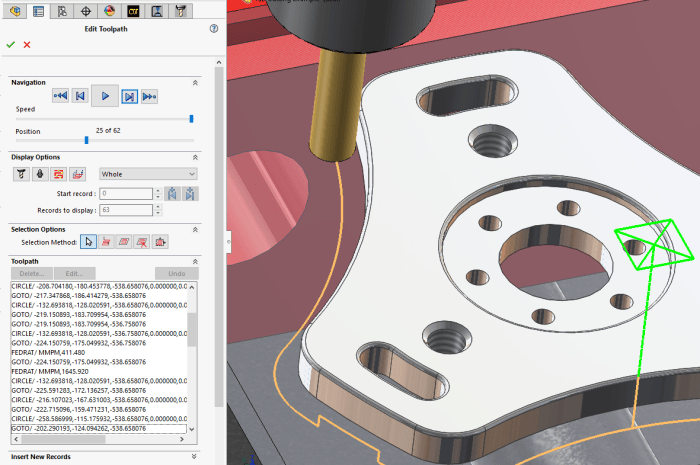
Source: g2crowd.com
When capital expenditures reach into six figures for enterprise-grade manufacturing software, business owners look far beyond raw cutting speeds. They examine the human element—how quickly a fresh graduate from a technical institute or a manual machinist can transition into a proficient digital programmer without stalling shop productivity. The financial return on investment hinges on minimizing downtime and accelerating the onboarding trajectory through structured educational pathways and adaptive software interfaces.
Deploying advanced computer-aided manufacturing platforms across a diverse workforce requires a blend of rigorous pedagogical frameworks and intuitive system architecture. Facilities that successfully scale their operations typically invest as much in human capital development as they do in software licensing. By bridging the gap between theoretical toolpath generation and practical chip-making reality, modern programming suites empower shops to bridge the skills gap, turning green operators into reliable assets who can safely push multi-axis machinery to its absolute limits.
Pedagogical frameworks for training novice programmers from scratch, Mastercam vs camworks
Transforming an absolute beginner into a competent programmer demands a systematic, phased educational blueprint that mirrors the actual complexity of modern machining. Educational institutions and corporate training centers increasingly rely on a competency-based curriculum that starts with fundamental geometric modeling and manual G-code interpretation before introducing automated feature recognition. This foundational step ensures that learners understand the underlying mathematics of cutter compensation and feed rate calculations rather than merely clicking buttons on an interface.
Subsequent phases introduce simulation-based environments where students can commit and rectify programming errors in a risk-free virtual space, observing the catastrophic results of a simulated gouge without damaging expensive alloy workpieces or multi-million-dollar CNC spindles. Advanced modules then guide trainees through real-world case studies, such as programming an intricate aerospace bracket with tight geometric tolerancing, thereby cementing their ability to balance cycle time optimization with surface finish integrity.
Ecosystem expansion through third-party modules and hybrid packages
The modern manufacturing landscape demands extreme versatility, pushing software developers and independent vendors to offer robust arrays of supplementary add-ons and specialized application packages. Facilities venturing into complex Swiss-style turning or simultaneous mill-turn operations often find that core software suites require dedicated modules to handle synchronized sub-spindle transfers and live-tooling kinematics effectively. Third-party tool management databases, automated deburring algorithms, and specialized additive manufacturing modules integrate seamlessly via robust application programming interfaces.
For instance, aerospace tier-one suppliers frequently integrate specialized airfoil machining packages that calculate specialized flank-milling toolpaths, drastically reducing programming time compared to standard multi-axis swarf routines.
Investing in specialized hybrid application packages transforms a standard milling center into a multi-tasking powerhouse, directly impacting the bottom line through reduced part handling and setup reduction.
Furthermore, adaptive control add-ons monitor spindle load in real time, dynamically altering feed rates to protect expensive carbide cutting tools when encountering unexpected material hard spots in titanium forgings.
Hardware specifications required for massive aerospace mold assemblies
Manipulating sprawling digital twins of commercial aircraft wing molds or large-scale composite tooling demands workstation hardware that pushes computing architecture to the bleeding edge. Graphical processing units equipped with dedicated ray-tracing cores and massive video random-access memory are mandatory to render millions of faceted triangles smoothly without stuttering during dynamic rotation. Central processing units featuring high single-core clock speeds combined with extensive multi-threaded capabilities ensure that complex toolpath calculations, such as steep-and-shallow finishing routines, compute in minutes rather than hours.
Enterprise-level workstations deployed in modern engineering bureaus typically feature a minimum of sixty-four gigabytes of error-correcting code random-access memory to prevent data corruption when loading assemblies containing tens of thousands of individual components. Storage architecture has similarly evolved, with high-speed non-volatile memory express solid-state drives operating on PCIe lanes becoming the industry standard for rapidly streaming massive point cloud data sets and simulation logs.
To mitigate physical fatigue and protect the physical well-being of programmers who spend long hours refining complex toolpaths, modern software suites provide extensive user interface personalization capabilities. Implementing these tailored workspace configurations significantly reduces repetitive strain injuries by streamlining daily mouse travel and keyboard interactions. Operations can leverage specific functional adjustments to optimize their physical interaction with the software:
- Customizable radial marking menus that position frequently used toolpath strategies directly under the cursor, reducing total daily mouse click counts by upwards of forty percent.
- Configurable keyboard shortcut panels mapped to ergonomic gaming peripherals, allowing operators to execute complex view manipulations and simulation replays without straining their wrists.
- High-contrast dark-mode color themes and scalable high-dpi font rendering options that minimize eye strain during extended night-shift programming sessions under harsh fluorescent shop lighting.
- Dockable, floating tool palettes that can be rearranged on multi-monitor setups to keep parameter dialog boxes within the user’s natural line of sight, eliminating awkward neck twists.
Last Word: Mastercam Vs Camworks
Navigating the complex landscape of modern computer-aided manufacturing ultimately boils down to aligning powerful software capabilities with your specific shop floor ambitions. Whether you lean toward boundless toolpath customizability or automated feature-recognition intelligence, both digital powerhouses offer incredible potential to elevate your machining operations. Embrace the journey of technological evolution, empower your programming team with the right tools, and watch your manufacturing enterprise soar to unprecedented heights of precision and profitability.
